
Browse our ISO-certified inventory of heavy-duty hex bolts, studs, socket cap screws, and specialty alloy fasteners manufactured for power generation, petrochemical plants, and heavy machinery.
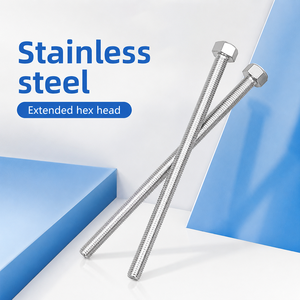
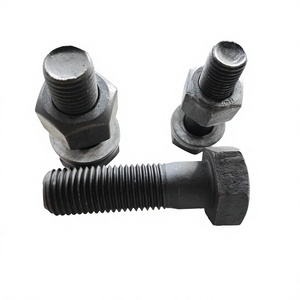
Why Chrome-Moly-Vanadium Steel remains the definitive standard for high-temperature pressure vessel and steam turbine flanging worldwide.
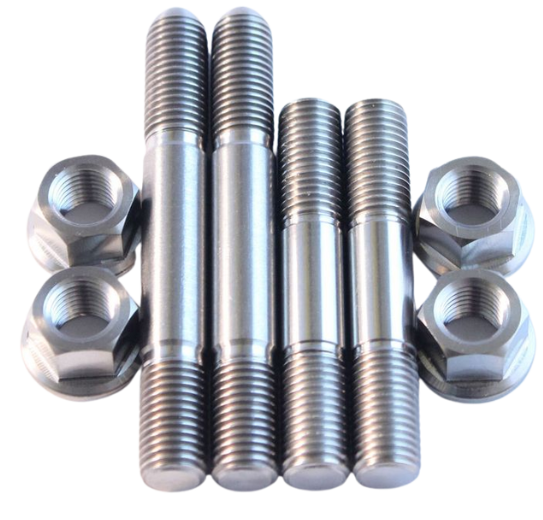
The standard ASTM A193 Grade B7 alloy steel stud bolt (Cr-Mo) is universally recognized for its robust tensile performance up to 425°C (800°F). However, when modern thermal processing units, combined-cycle gas power plants, and ultra-supercritical steam turbines operate consistently between 450°C and 550°C (840°F – 1020°F), standard B7 bolts experience significant thermal creep relaxation, loss of clamping force, and potential flange gasket joint leakage.
ASTM A193 Grade B16 addresses this high-temperature boundary by incorporating controlled additions of Vanadium (0.25% – 0.35%) into the Chromium-Molybdenum steel matrix. During precise heat treatment (hardening followed by tempering at a minimum temperature of 650°C / 1200°F), vanadium forms fine, thermally stable vanadium carbides ($V_4C_3$) precipitated throughout the grain boundaries. These micro-carbides pin dislocation movement, dramatically improving long-term creep rupture strength and resisting stress relaxation under extreme thermal loads.
As a leading Chinese manufacturer and global exporter, our ASTM A193 B16 stud bolts undergo rigorous ladle analysis and mechanical testing in strict compliance with ASTM A193/A193M and ASME SA193 specifications.
| Specification Parameter | ASTM A193 Grade B16 (Cr-Mo-V) | ASTM A193 Grade B7 (Cr-Mo) | ASTM A453 Grade 660 (Class A/B) |
|---|---|---|---|
| Primary Element Alloy | Chromium-Moly-Vanadium | Chromium-Molybdenum | Iron-Nickel-Chromium-Titanium |
| Operating Temp Limit | Up to 550°C (1020°F) | Up to 425°C (800°F) | Up to 570°C – 650°C (1200°F) |
| Tensile Strength (Min.) | 125 ksi (860 MPa) [≤ 2.5"] | 125 ksi (860 MPa) [≤ 2.5"] | 130 ksi (895 MPa) |
| Yield Strength 0.2% (Min.) | 105 ksi (725 MPa) [≤ 2.5"] | 105 ksi (725 MPa) [≤ 2.5"] | 85 ksi (585 MPa) |
| Vanadium (V) Content | 0.25% – 0.35% | None | 0.10% – 0.50% |
| Molybdenum (Mo) Content | 0.50% – 0.65% | 0.15% – 0.25% | 1.00% – 1.50% |
| Companion Heavy Hex Nut | ASTM A194 Grade 4 or Grade 7 | ASTM A194 Grade 2H or Grade 7 | ASTM A453 Grade 660 / A194 Gr 8M |
We deliver full end-to-end manufacturing oversight from raw steel bar billet inspection to precision CNC thread rolling, heat treatment, and anti-corrosion coating.
Our continuous computer-controlled heat-treatment furnaces perform precise liquid quenching (oil/water) followed by high-temperature tempering above 650°C. This guarantees a uniform tempered martensite grain structure free of untempered residual stresses.
Every batch of ASTM A193 B16 studs undergoes positive material identification (PMI spectro testing), Charpy V-notch impact testing at low/ambient temperatures, hardness profile testing (HBW/HRC), axial tensile tests, and thread pitch micrometer checks.
High-temperature bolting requires specialized surface barrier coatings to eliminate thread galling during hot disassembly. We supply fluoropolymer (PTFE / Xylan 1014/1424), Zinc-Nickel (Zn-Ni) electroplating, Hot-Dip Galvanizing (HDG), and Phosphate coating solutions.
Navigating energy transition demands, stringent global decarbonization standards, and digital supply chain integration for critical infrastructure.
As thermal power plants transition toward higher thermal efficiencies and integrate green hydrogen or ammonia co-firing, operational steam temperatures exceed traditional limits. Procurement trends show a rapid shift from standard B7 bolts toward ASTM A193 B16 and Nickel Alloy 625/718 to withstand enhanced hydrogen embrittlement risks and higher cyclic creep stresses without joint failure.
Modern EPC contractors and refinery operators no longer accept static paper certificates. Supply chains now demand digital material passports with micro-stamped QR codes directly on fastener end faces. This links each stud bolt in the field directly to its EN 10204 3.1 chemical ladle analysis, heat treatment chart, and ultrasonic non-destructive test (NDT) records instantly.
To mitigate volatile raw material pricing and extended lead times, global buyers are consolidating fastener purchases with fully integrated Chinese manufacturers. Direct mill sourcing guarantees reliable billet supply, large-scale automated forging capacity, and short lead times for custom thread pitches (8UN, UNC, UNF, Metric pitch) and non-standard stud lengths.
ASTM A193 B16 alloy steel stud bolts and heavy hex nuts are mandatory components across energy-intensive industries where bolt failure can lead to catastrophic pressure loss or environmental contamination:
Clear technical answers to help purchasing agents, quality inspectors, and piping engineers select the exact ASTM A193 B16 bolting specifications.
Partner with China’s premier high-temperature alloy fastener manufacturer. Submit your detailed material schedule, drawings, thread pitch, coating specs, and destination port for an immediate competitive factory-direct quote.