
Explore our certified range of industrial stud bolts, heavy hex nuts, marine-grade fasteners, and specialized OEM alloy bolting components manufactured to rigid ASME, ASTM, and DIN standards.
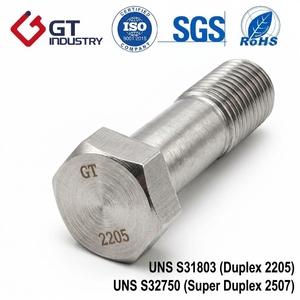
NACE MR0175 compliant for offshore piping, resisting chloride stress corrosion cracking under high-pressure thermal cycles.
Precision-machined SS304/SS316 M2-M30 industrial hexagon nuts with anti-galling black oxide chemical conversion treatment.
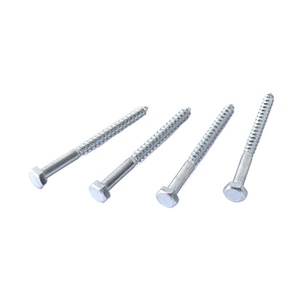
Heavy-duty marine engine maintenance durability bolt sets engineered to resist salt fog ambient degradation and mechanical wear.
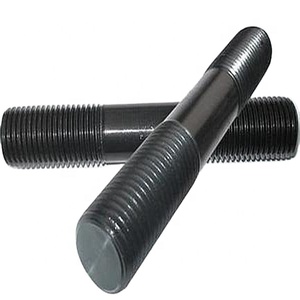
100% hardness tested low-alloy steel stud and heavy nut sets tailored specifically for sour gas service and refinery pressure vessels.
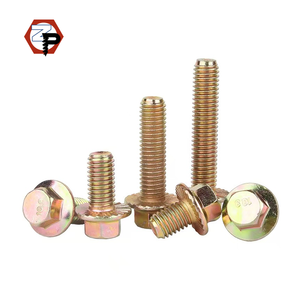
M12-M16 custom OEM sizing featuring anti-vibration bottom serrations to maintain clamp load in vibrating industrial machinery.
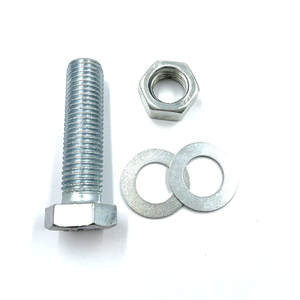
Hot-dip galvanized high-tensile structural nut kits utilized extensively in petrochemical towers and power station steel structures.
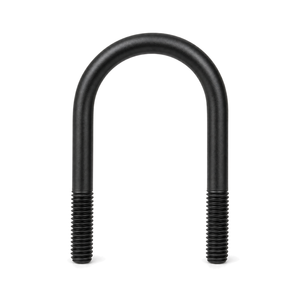
Black oxide & stainless steel (304/Carbon) double head UNF threaded U-bolt assemblies engineered for pipe support systems.
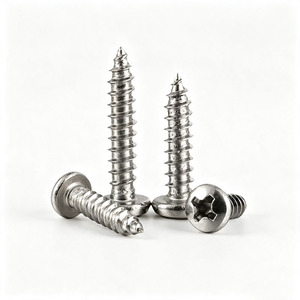
M3-M6 deep-thread corrosion-resistant pan head screws manufactured for electrical enclosures and precision industrial assemblies.
ASTM A193 Grade B7 represents the global gold standard for high-tensile bolting in pressure vessels, valves, flanges, and fittings. Metallurgically, Grade B7 is a heat-treated chromium-molybdenum low-alloy steel based on AISI 4140/4142 chemical composition. Through precise liquid quenching (in oil or water) followed by tempering at a minimum temperature of 1100°F (593°C), Grade B7 attains superior tensile strength, yield resilience, and elevated temperature creep resistance up to 450°C (840°F).
For chemical plant operators, refinery engineers, and EPC contractors, ensuring strict adherence to the mechanical and elemental limits specified under ASTM A193 is vital for structural integrity. Below is the chemical and mechanical property matrix engineered into every heat batch at our custom OEM facility.
| Element / Parameter | ASTM A193 B7 Specification | ASTM A193 B7M (Sour Service) | ASTM A193 Grade B16 |
|---|---|---|---|
| Carbon (C) | 0.37 - 0.49 % | 0.37 - 0.49 % | 0.36 - 0.47 % |
| Chromium (Cr) | 0.75 - 1.20 % | 0.75 - 1.20 % | 0.80 - 1.15 % |
| Molybdenum (Mo) | 0.15 - 0.25 % | 0.15 - 0.25 % | 0.50 - 0.65 % |
| Vanadium (V) | N/A | N/A | 0.25 - 0.35 % |
| Min. Tensile Strength | 125 ksi (860 MPa) [≤ 2.5"] | 100 ksi (690 MPa) | 125 ksi (860 MPa) [≤ 2.5"] |
| Min. Yield Strength (0.2%) | 105 ksi (720 MPa) [≤ 2.5"] | 80 ksi (550 MPa) | 105 ksi (720 MPa) [≤ 2.5"] |
| Max. Hardness | 321 HBW / 35 HRC | 235 HBW / 22 HRC (NACE) | 321 HBW / 35 HRC |
| Operating Temp Range | -29°C to 450°C (-20°F to 840°F) | -29°C to 450°C (Sour Environment) | -29°C to 525°C (Up to 975°F) |
When selecting stud bolts for critical pressure-retaining flanges under ASME B16.5, ASME B16.47, or API 6A standards, matching the stud bolt grade with the corresponding heavy hex nut (such as ASTM A194 Grade 2H or Grade 2HM) is critical to prevent thread stripping under intense bolt tension.
As an ISO 9001:2015 certified manufacturer based in Mumbai, our production facility combines advanced CNC machining, high-speed thread rolling mills, and automated continuous thermal treatment furnaces. The structural durability of an ASTM A193 B7 stud bolt depends heavily on how the thread profile is manufactured.
Thread rolling re-orients metal grain lines continuously along the thread contour, creating compressive residual stress that increases fatigue resistance by up to 300% compared to machine-cut threads.
Computerized oil-quenching tanks prevent micro-cracking and thermal distortion, ensuring homogenous martensitic grain structure across large-diameter stud rods up to M100 / 4 inches.
For wet H2S oilfield applications, our ASTM A193 Grade B7M stud bolts undergo 100% micro-hardness inspection to guarantee hardness below 22 HRC, preventing Sulfide Stress Cracking (SSC).
Custom OEM manufacturing allows us to tailor thread pitch standard specifications (UN8 single-point / multi-point unified constant pitch series vs. UNC coarse threads), shank length, chamfer geometry, and non-standard collar designs according to specific engineering blueprints.
Untreated alloy steel fasteners succumb rapidly to atmospheric rust, marine splash-zone oxidation, and chemical vapor attack. To extend service lifespan and prevent severe bolt galling during installation and breakout maintenance, we provide specialized surface treatments engineered for aggressive operating environments:
Delivers exceptional low coefficient of friction (0.05-0.08), eliminating torque loss during tightening and offering 1500+ hours salt spray resistance.
Conforming to ASTM A153, HDG yields a thick zinc sacrificial layer (≥50 µm) for heavy structural, electrical utility, and power plant installations.
Electro-deposited 12-15% Ni alloy plating providing superior heat barrier protection up to 300°C without hydrogen embrittlement risks.
Traditional low-friction anti-galling coatings specified for aerospace, defense, and high-precision torque-critical applications.
The industrial fastener market is undergoing a structural evolution driven by clean energy transition, digital supply chain integration, and stringent regulatory demands. Procurement leaders must align with forward-thinking custom OEM manufacturers to mitigate risk and secure long-term project profitability.
We bridge the gap between heavy industrial engineering demands and seamless international B2B procurement logistics.
Every single stud bolt is deep-stamped with material grade, manufacturer identification mark, and heat number, backed by EN 10204 3.1 certification detailing chemical heat analysis and physical test results.
Equipped with optical emission spectrometers (PMI), Universal Testing Machines (UTM) for tensile/yield verification, Charpy impact testers, Rockwell/Brinell hardness testers, and salt spray fog chambers.
From custom length engineering studs, double-end step studs, and reduced shank body bolts to unique thread pitches, our engineering team manufactures directly from your CAD drawings.
Export shipments are treated with VCI (Vapor Corrosion Inhibitor) oil spray, individually wrapped, packed into heavy-duty fumigated wooden crates, and palletized for safe ocean freight delivery across 24+ countries.
Situated in Mumbai, India, our proximity to major international seaports (Nhava Sheva / JNPT) allows rapid container consolidation and shortened shipping transit times to the Middle East, Europe, and the Americas.
Consolidate your entire order—stud bolts, heavy hex nuts, flat washers, spring lock washers, and cut-to-length threaded rods—under one unified quality control umbrella and single shipping invoice.
Technical and commercial clarity for procurement specialists, piping engineers, and QA inspectors.
Connect directly with our technical sales team in Mumbai. We provide rapid price quotations, chemical-mechanical compatibility guidance, and full product catalogs tailored for your specific project requirements.