
Engineered to international quality metrics (ASTM, DIN, ISO, ANSI) with full heat-batch traceability and certified anti-corrosion barrier coatings.
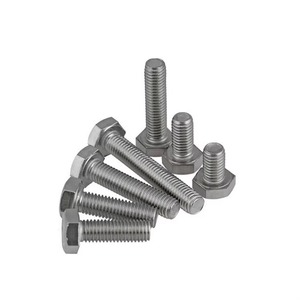
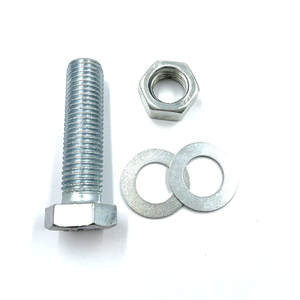
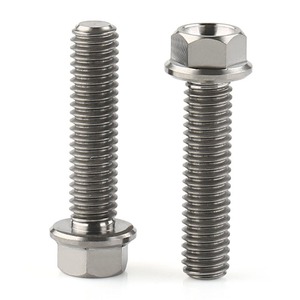
Understanding the Iron-Zinc Alloy Phase Transformation, Grain Boundary Diffusion, and Cathodic Protection in Harsh Industrial Environments.
Hot Dip Galvanizing (HDG) is not merely a surface coating; it is a chemical diffusion process resulting in a metallurgical bond between molten zinc and structural carbon/alloy steel. When steel fasteners or structural fabrications are immersed in molten zinc at approximately 450°C (840°F), a reaction forms a series of zinc-iron alloy layers covered by a outer layer of pure zinc.
These distinct microstructural phases grant HDG its exceptional physical hardness and corrosion resistance:
A critical engineering parameter controlled at our OEM factory is managing steel chemistry—specifically Silicon (Si) and Phosphorus (P) content. Steel containing Si between 0.04% and 0.14% or exceeding 0.25% exhibits hyper-reactivity (the Sandelin Effect), causing rapid Zeta-phase growth and brittle, matte-grey coatings.
Our OEM metallurgists pre-screen raw steel billets via Optical Emission Spectrometry (OES) to balance Si-P stoichiometry, guaranteeing uniform coating thickness, optimal ductility, and strict compliance with ASTM A123/A123M and ASTM A153/A153M.
Coating Thickness: 45 μm – 150+ μm
Bond Type: Metallurgical Alloy Fusion
Cathodic Protection: Exceptional (Sacrificial)
Salt Spray Lifespan: > 1,500 Hours to First Red Rust
Best For: Heavy Infrastructure, Petrochemical, Marine & High Tensile Fasteners.
Coating Thickness: 5 μm – 12 μm
Bond Type: Mechanical Deposition
Cathodic Protection: Minimal / Short-Term
Salt Spray Lifespan: 48 – 96 Hours
Best For: Indoor Hardware, Automotive Trim & Non-Corrosive Assembly.
Coating Thickness: 15 μm – 45 μm
Bond Type: Zinc Vapor Diffusion
Cathodic Protection: Moderate
Salt Spray Lifespan: ~500 Hours
Best For: Complex Internal Threaded Components & Precision Pressings.
Comprehensive standard compliance metrics across dimensional tolerances, mechanical properties, and environmental exposure limits.
| Specification Standard | Applicable Material Grades | Min. Coating Weight (g/m²) | Coating Thickness (μm) | Salt Spray Resistance (ASTM B117) | Thread Over-Tapping Class |
|---|---|---|---|---|---|
| ASTM A153 Class C | Fasteners & Threaded Items (>3/8 in) | 381 g/m² | 54 μm | 1,200+ Hours | UNC 2A / 3A (Over-tapped 2B/3B Nut) |
| ASTM A153 Class D | Rolled Threads, Washers, Small Items | 305 g/m² | 43 μm | 1,000+ Hours | Unified Extra Fine (UNEF / Pitch Adj.) |
| ASTM F2329 | Carbon & Alloy Steel Bolts / Nuts | 350 g/m² | 50 μm | 1,500+ Hours | ISO Metric (6G / 6H Oversized) |
| ISO 1461 (Batch HDG) | Steel Fabrications & Structural Steel | 610 g/m² | 85 μm | 2,000+ Hours | N/A (Structural Members) |
| ASTM A193 B7 / B16 | High-Temp / High-Pressure Stud Bolts | 400 g/m² (Spin HDG) | 55 μm | 1,500+ Hours (baked) | Special Pitch Allowance per ASME B1.1 |
| Grade 10.9 / 12.9 High Tensile | Alloy Steel Structural Fasteners | 381 g/m² | 54 μm | 1,500+ Hours | Mandatory De-Embrittlement Baked |
Our fully automated centrifugal hot-dip galvanizing lines guarantee thread precision and eliminate zinc pooling on heavy hex nuts and studs.
Multi-stage immersion cleaning: Hot Alkaline Degreasing removes oils; Hydrochloric Acid (HCl) Pickling removes scale; Zinc Ammonium Chloride (ZAC) Fluxing prevents pre-oxidation before dipping.
Fasteners are submerged in 99.995% pure molten zinc at 445°C–455°C. High-speed centrifugal spinners immediately evacuate excess molten zinc from internal and external thread profiles.
Rapid liquid quenching preserves grain structure while liquid sodium dichromate or chromium-free passivating dip halts white rust (zinc storage stain) formation during overseas container transit.
For high-strength steel grades (≥ 1000 MPa tensile strength, e.g., Grade 10.9, 12.9, ASTM A193 B7), fasteners undergo immediate thermal baking at 190°C–210°C for 4 to 24 hours per ASTM F519 to eliminate Hydrogen Embrittlement risk.
100% thread gauge verifications using GO / NO-GO ring and plug gauges. Nuts are precisely over-tapped post-galvanizing to accommodate the coating thickness on bolt threads without sacrificing stripped-load capacity.
Every export shipment includes comprehensive inspection certificates detailing chemical heat analysis, mechanical tensile strength, proof load, coating thickness (Magna-Gage), and salt spray test results.
Market intelligence and technological evolutions reshaping global industrial fastener sourcing, environmental compliance, and life-cycle economics.
Global EPC contractors and OEM buyers are implementing strict Scope 1, 2, and 3 carbon reduction mandates. Future procurement favors galvanizing plants utilizing natural gas regenerative burner furnaces, enclosed diffusion kettles, and primary zinc produced via zero-carbon hydro-electric smelting.
Our factory lead in adopting recycled zinc recovery loops, achieving a 30% reduction in carbon footprint per metric ton of processed fasteners.
For extreme offshore marine, subsea, and H2S sour gas refineries (NACE MR0175 compliance), standard HDG alone is being upgraded to Duplex Coating Systems. This process applies a secondary fluoropolymer (PTFE/Xylan) or ceramic barrier topcoat directly over hot-dip galvanized surfaces.
The synergic duplex effect extends service life by 1.5 to 2.5 times compared to the sum of individual coatings, resisting C5-M marine exposure for up to 50 years.
Manual thread gauging is rapidly giving way to 3D laser profiling and high-speed vision sorting lines. Future global procurement requirements will mandate 100% automated optical inspection (AOI) to eliminate thread galling, micro-cracks, and coating unevenness in high-speed automated assembly plants.
Geopolitical shifts and freight volatility are driving Tier-1 procurement teams toward integrated OEM factories with robust raw material reserves and end-to-end manufacturing (forging, heat treatment, galvanizing, packaging) under one roof, reducing lead times from months to weeks.
Combining world-class metallurgical expertise with flexible custom manufacturing to support your most demanding engineering projects.
We manufacture custom non-standard fasteners, anchor bolts, stud bolts, and structural components directly from customer CAD drawings and technical specifications.
In-house testing facility equipped with Spectrometers, Universal Tensile Machines (UTM), Charpy Impact Testers, Hardness Testers (HRC/HBW), and Salt Spray Chambers.
VCI anti-corrosion film wrapping, heavy-duty wooden crates, fumigated ISPM-15 wooden pallets, and steel band strapping ensure products arrive pristine.
Expert answers addressing thread engagement, standards compliance, coating thicknesses, and Hydrogen Embrittlement mitigation.
Partner with an ISO 9001:2015 certified manufacturer. Connect with our engineering team for immediate pricing, sample dispatch, and custom drawing reviews.