
Call: +91 91723 33437 Email: [email protected] Address: Mumbai, India
Industry Procurement Whitepaper 2025

Top 10 Zinc Plated Fasteners Manufacturer & Suppliers

Comprehensive Technical Analysis, Metallurgical Compliance, and Global Supply Chain Evaluation for High-Strength Fastening Solutions

Featured Zinc Plated Fastener Product Portfolio

Engineered for high-tensile reliability, corrosion resistance, and ISO/ASTM compliance across marine, energy, and heavy construction sectors.
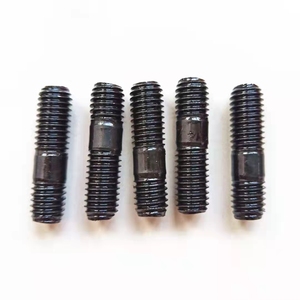
High Strength Carbon Steel Double Threaded End Stud Bolts Nuts Washers High Quality Zinc Finish M8 Size M16 M27 140mm 120mm
ASTM A193 B7 / Carbon Steel

High Strength Carbon Steel Double Threaded End Stud Bolts Nuts Washers High Quality Zinc Finish M8 Size M16 M27 140mm 120mm

Precision double-end studs engineered with sacrificial zinc electro-coating (5-12µm thickness). Designed for flange bolting in pressure vessels and heavy equipment assemblies requiring high tensile yield strength.
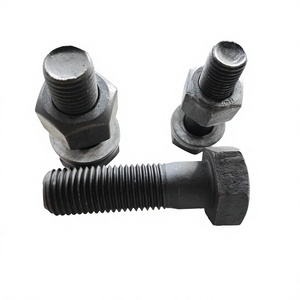
High Tensile Steel Hex Bolt Industrial Grade Mechanical Fastener For Construction Machinery And Equipment
Grade 8.8 / 10.9 Mechanical

High Tensile Steel Hex Bolt Industrial Grade Mechanical Fastener For Construction Machinery And Equipment

Heavy-duty hex head bolts compliant with ISO 4014 / DIN 931. Features clear trivalent zinc passivation for enhanced rust prevention in heavy construction gear and dynamic loading structures.
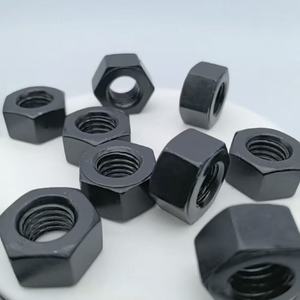
Zinc Plated Black Oxide ASTM A194 2H Alloy Steel Hex Nuts High Strength Grade 8.8 10.9 12.9 Fasteners for Oil Gas Heavy Industry
ASTM A194 Grade 2H / 2HM

Zinc Plated Black Oxide ASTM A194 2H Alloy Steel Hex Nuts High Strength Grade 8.8 10.9 12.9 Fasteners for Oil Gas Heavy Industry

Quenched and tempered heavy hex nuts featuring dual surface protection (Zinc electroplate over black oxide barrier). Formulated specifically to eliminate thread galling in high-pressure oil & gas piping environments.
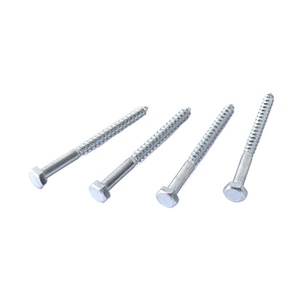
Coastal Environment Fasteners SUS304 Hex Head Bolt Kit for Offshore Platform Equipment and Marine Engine Maintenance Durability
Marine Grade AISI 304 / A2

Coastal Environment Fasteners SUS304 Hex Head Bolt Kit for Offshore Platform Equipment and Marine Engine Maintenance Durability

Austenitic stainless steel bolt kits backed with secondary anti-seize zinc passivation. Tested under ASTM B117 salt spray chambers exceeding 720 hours without red rust, ideal for offshore platform rigs.
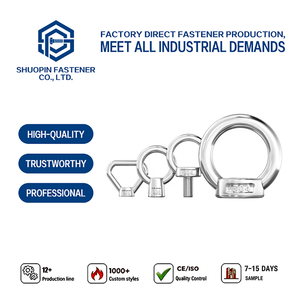
Petroleum Chemical Plant Seawater Desalination Port Ship 316 Stainless Steel DIN582 Lifting Eye Nut Corrosion Resistant Fastener
AISI 316 / DIN 582 Rigging

Petroleum Chemical Plant Seawater Desalination Port Ship 316 Stainless Steel DIN582 Lifting Eye Nut Corrosion Resistant Fastener

Molybdenum-alloyed metric drop-forged lifting eye nuts. Designed for critical load-bearing operations in chemical process plants and desalination facilities exposed to aggressive chloride concentrations.
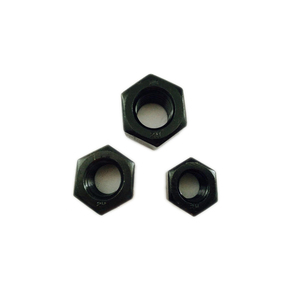
Heavy Duty Nuts Black Astm A194 Gr 2h Nut
ASTM A194 2H High Temp

Heavy Duty Nuts Black Astm A194 Gr 2h Nut

Carbon steel heavy hex nuts heat-treated for elevated pressure and high-temperature service. Available with custom electro-zinc or phosphated protective finishes for refinery manifold bolting.
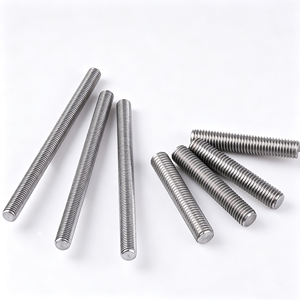
Stainless Steel DIN975 Full Threaded Rod Stud Bolt Anti Corrosion High Tensile For Construction
DIN 975 / DIN 976 Studs

Stainless Steel DIN975 Full Threaded Rod Stud Bolt Anti Corrosion High Tensile For Construction

Continuous fully threaded bars available in 1-meter to 3-meter lengths. Roll-threaded for superior fatigue strength in anchor bolting, MEP pipe support hangers, and structural concrete framing.
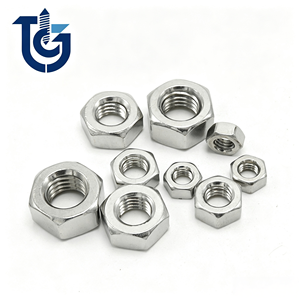
304 316 Stainless Steel Hex Nuts DIN934 Metric Hex Nut For Bolts Factory Wholesale Custom Available
DIN 934 / ISO 4032 Standard

304 316 Stainless Steel Hex Nuts DIN934 Metric Hex Nut For Bolts Factory Wholesale Custom Available

Standard metric hex nuts manufactured to precise pitch tolerances. Available with yellow zinc dichromate or trivalent clear coating to meet diverse OEM assembly specifications.

24+
Global Export Markets
1000+
SST Hours Resistance (Zn-Ni)
ISO 9001
Certified Quality Management
EN 10204 3.1
Traceable Mill Certification

Technical Executive Summary: Evaluating the Global Zinc Plated Fastener Landscape

In high-stakes industrial engineering—spanning petro-chemical processing, subsea oil exploration, structural steel construction, and heavy automotive manufacturing—the selection of threaded fasteners is never merely a commoditized purchasing decision. Fasteners represent critical single-point failure vectors. Among surface protection technologies, zinc plated fasteners remain the global benchmark for combining cost-effective sacrificial corrosion resistance, precise thread pitch tolerances, and aesthetic surface consistency.

This technical whitepaper provides B2B procurement managers, metallurgical engineers, and EPC contractors with an exhaustive evaluation framework for selecting high-strength zinc-plated stud bolts, heavy hex nuts, threaded rods, and specialized socket screws. By synthesizing empirical field data, international standards (ASTM A193, ASTM A194, ASTM F1941, ISO 4042, DIN 934), and manufacturing quality controls, this guide establishes clear procurement benchmarks aimed at mitigating premature hydrogen embrittlement, stress corrosion cracking (SCC), and atmospheric degradation.

Enterprise Manufacturing & Quality Engineering Standards

Why leading EPC contractors and global OEMs partner with audited Mumbai manufacturing facilities for critical bolting projects.

Hydrogen Embrittlement Mitigation

High-tensile fasteners (Property Class 10.9, 12.9, and ASTM A193 B7) undergo mandatory de-hydrogenation baking at 190°C–220°C for 4 to 24 hours within 4 hours of electroplating, adhering strictly to ASTM B849/B850 standards.

Cr6+ Free Trivalent Passivation

Fully compliant with global EU RoHS and REACH directives. Our automated electro-plating lines utilize environmentally safe Trivalent Chromium (Cr3+) passivates combined with silica topcoats for superior salt spray longevity.

100% Heat-Number Traceability

Every shipment is backed by EN 10204 3.1 Material Test Certificates (MTC), detailing spectrographic chemical composition, tensile yield tests, Charpy V-notch impact values, and micro-hardness testing.

Comparison Matrix: Electro-Zinc Plating vs. Alternative Industrial Coatings

When selecting surface treatments for industrial fasteners, engineers must weigh corrosion resistance, coating thickness, thread tolerance interference, and cost efficiency:

Coating Technology Standard Coating Thickness ASTM B117 Salt Spray (Red Rust) Thread Pitch Interference Risk Typical Industrial Application
Electro-Galvanized (Clear / Yellow Zinc) 5 µm – 15 µm 96 – 240 Hours Negligible (Fits 6g/6H) General Machinery, Structural Steel, Indoor Pipe Hangers
Zinc-Nickel Electroplate (88/12 Zn-Ni) 8 µm – 15 µm 720 – 1,000+ Hours Very Low Automotive Underbody, Offshore Oil & Gas, Marine Engines
Hot-Dip Galvanizing (HDG - ASTM A153) 45 µm – 85 µm 500 – 1,000 Hours High (Requires Over-tapping) Outdoor Transmission Towers, Highway Guardrails
PTFE / Xylan Fluoropolymer Coating 15 µm – 25 µm 1,000 – 3,000 Hours Moderate Subsea Flanges, Highly Acidic Chemical Processing

Strategic Procurement & Future Development Trends (2025–2030)

Key technological shifts shaping the global industrial fastener manufacturing sector and purchasing strategies.

1. Accelerated Shift Toward Zinc-Nickel (Zn-Ni) Alloy Coatings

As environmental regulations tighten around cadmium electroplating and hot-dip galvanizing energy consumption, the global fastener market is experiencing a rapid transition toward Zinc-Nickel alloy plating (85-88% Zn / 12-15% Ni). Offering five times the sacrificial protection of standard electro-zinc at comparable coating thicknesses, Zn-Ni eliminates thread pitch binding while providing thermal stability up to 300°C.

2. Total De-carbonization & Green Fastener Supply Chains

Tier-1 EPC contractors in Western Europe and North America now demand scope 3 carbon footprint disclosures for raw steel procurement. Manufacturing hubs in Mumbai are integrating green electric induction furnaces, solar-powered electro-plating tanks, and closed-loop chemical recycling systems to reduce the embodied carbon of exported fasteners.

3. Smart Fasteners & RFID Integrated Quality Tracking

The integration of micro-laser etched DataMatrix barcodes and heat-resistant RFID tags onto stud bolt end faces is revolutionizing digital inventory management. Maintenance teams in offshore oil fields can scan assembled stud bolts in real-time to pull up original heat numbers, torque specs, and coating inspection certificates.

4. Nearshoring & Regional OEM Hub Stocking

Global supply chain volatility has driven major industrial buyers to implement vendor-managed inventory (VMI) frameworks. Indian fastener exporters are establishing strategic regional warehousing hubs across the GCC region (UAE, Saudi Arabia, Qatar) and Rotterdam to provide 48-hour delivery windows for critical refinery turnarounds.

Engineering Selection Guide: Thread Fits, Tolerances, and Plating Thicknesses

A critical pitfall in mechanical design occurs when engineers specify heavy electro-plating thicknesses on standard ISO metric (6g/6H) or Unified Imperial (2A/2B) thread fits without calculating pitch diameter allowance. According to ASTM F1941 / ISO 4042, electro-deposited zinc builds up unevenly on threaded profiles—accumulating approximately twice as fast on crests and flanks compared to thread roots.

Standard Plating Thicknesses (ISO 4042)

  • Fe/Zn 5 (5 µm): Light indoor duty, electrical enclosures. Minimum allowance required.
  • Fe/Zn 8 (8 µm): Standard industrial machinery, mild outdoor exposure.
  • Fe/Zn 12 (12 µm): Heavy industrial equipment, outdoor architectural steel framing.
  • Fe/Zn 25 (25 µm): Severe atmospheric duty (Requires thread undercut before plating).

Passivation Chromate Options

  • Code A (Clear / Blue Trivalent): Aesthetic silvery finish; 24-48 hrs to white corrosion.
  • Code C (Yellow Iridescent): Enhanced barrier film; 72-120 hrs to white corrosion.
  • Code D (Black Passivate): Used extensively in optical & automotive underhood assemblies.
  • Code F (Olive Drab): Military-grade thick film passivation for extreme outdoor weathering.

Frequently Asked Questions (B2B Procurement FAQ)

Addressing essential technical, quality assurance, and international logistics queries for project buyers.

Which specific material grades do you manufacture for high-strength zinc plated fasteners? +
We manufacture and export zinc plated fasteners across a complete spectrum of material grades. This includes High Tensile Carbon & Alloy Steels (ASTM A193 Grade B7, B7M, B16, ASTM A320 Grade L7, Property Class 8.8, 10.9, 12.9), Heavy Hex Nuts (ASTM A194 Grade 2H, 2HM, 4, 7, 8, 8M), Stainless Steels (AISI 304, 316, 316L, 321, 347), Duplex & Super Duplex (UNS S31803, S32205, S32750, S32760), and Nickel Superalloys (Inconel 625/718, Monel 400/K-500, Hastelloy C276).
How does electro-zinc plating prevent atmospheric corrosion compared to Hot-Dip Galvanizing (HDG)? +
Electro-zinc plating deposits a uniform, smooth layer of metallic zinc (typically 5 to 15 microns) via electrolytic deposition. Zinc acts as a sacrificial anode, corroding preferentially to protect the underlying steel substrate. While Hot-Dip Galvanizing deposits a much thicker zinc coating (45 to 85+ microns), it creates rough surfaces and requires over-tapping of nut threads. Electro-zinc plating ensures exact pitch diameter compliance for precision metric and imperial threads without requiring thread chasing.
What mandatory precautions are taken to prevent Hydrogen Embrittlement in Grade 10.9 / ASTM A193 B7 fasteners? +
High-tensile fasteners with hardness levels exceeding 32 HRC (or core tensile strengths over 1000 MPa) are highly susceptible to Hydrogen Embrittlement (HE) during acid pickling and electro-plating. Our ISO-certified quality protocol mandates that all high-strength fasteners undergo a de-hydrogenation baking process at 190°C to 220°C for a minimum of 4 to 24 hours immediately following electro-deposition (within a 4-hour window), strictly conforming to ASTM B849, ASTM B850, and ISO 4042 guidelines.
What certification and quality documentation are supplied with export shipments? +
Every international shipment is delivered with comprehensive quality dossier compliance, including EN 10204 Type 3.1 Material Test Certificates (MTC). Documentation covers spectrographic chemical composition, mechanical tensile and yield strength, elongation percentage, core and surface hardness testing (Rockwell/Vickers), coating thickness reports (X-ray fluorescence testing), ASTM B117 salt spray test logs, and complete heat-number melt-to-mill traceability reports. Third-party inspection (TPI) by Lloyds, Bureau Veritas, or TÜV is available upon request.
Can custom dimensions, special thread pitches, and non-standard stud lengths be manufactured to drawing? +
Yes. In addition to standard metric (DIN 931, DIN 933, DIN 934, DIN 975) and imperial (ASME B18.2.1, ASME B18.2.2, ASME B18.31.2) fasteners, our Mumbai manufacturing facilities feature CNC turning and hot-forging capabilities to produce custom engineered fasteners. We fabricate non-standard lengths, step-down studs, special thread pitches (UNJ, Fine Metric, BSW), and custom flange hex bolts directly to client-supplied engineering drawings.
What are your standard export packaging protocols for ocean freight delivery? +
To guarantee zero surface corrosion or thread impact damage during ocean transport across 24+ export destinations, fasteners are packed using heavy-duty VCI (Vapor Corrosion Inhibitor) poly-bags inside double-walled corrugated cartons (25kg net limit per box). Cartons are heat-sealed, stacked on fumigated ISPM-15 wooden pallets, shrink-wrapped with stretch film, and bound with heavy plastic strapping for seaworthy shipping container transport.

Request an Immediate Technical Quotation & Sample Kit

Partner with an ISO-certified industrial fastener manufacturer. Submit your detailed material specifications, size requirements, thread pitches, and target delivery timelines today.