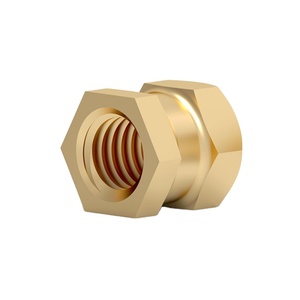

Explore our factory-direct heavy hex nuts manufactured in stainless steel, high-tensile carbon steel, brass, and exotic alloys. Designed for high-stress applications across oil & gas, marine, and power generation.
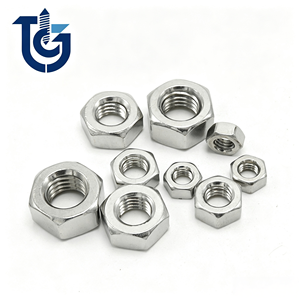
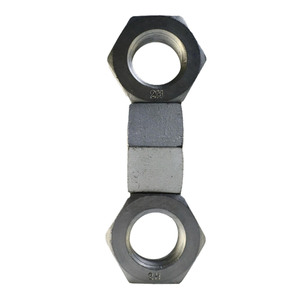
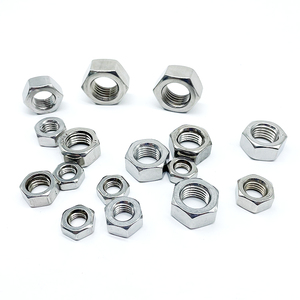
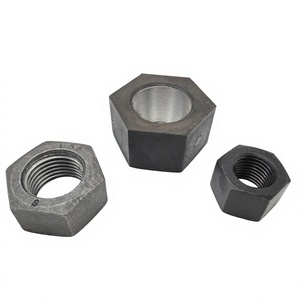
When procuring industrial fasteners for high-load pressure vessels, heat exchangers, subsea pipelines, and heavy industrial equipment, selecting the correct nut geometry and material grade is critical for structural integrity. As a premier China Heavy Hex Nuts Factory & Supplier, our engineering department adheres strictly to ASME B18.2.2, ASTM A194, and DIN standards to prevent premature thread stripping, stress corrosion cracking (SCC), and joint relaxation.
Heavy hex nuts differ fundamentally from standard finished hex nuts (such as ANSI B18.2.1 or ISO 4032) in both dimensional proportions and load-bearing performance. A heavy hex nut possesses a greater width across flats (WAF) and slightly increased thickness. This extra material enlarges the bearing surface area, distributing clamping force across a larger section of the mated flange or structure and significantly decreasing bearing stress under high bolt tensions.
Heavy hex nuts feature approximately 1/8 inch larger across-flats width than standard hex nuts of equivalent nominal diameter. This increased geometry directly impacts stress distribution:
Our manufacturing facility produces heavy hex nuts across all major ASTM and ISO material classifications:
| Standard Specification | Material Grade | Size Range | Proof Load Stress (PSI) | Surface Finish Options | Primary Application |
|---|---|---|---|---|---|
| ASTM A194 / A194M | Grade 2H / 2HM | 1/4" to 4" (M6 - M100) | 175,000 PSI (up to 1.5") | Black Oxide, HDG, PTFE, Zinc-Nickel | Oil & Gas Flanges, Pressure Vessels |
| ASTM A194 / A194M | Grade 8 / 8M (Class 1 & 2) | 1/4" to 3" (M6 - M76) | 80,000 to 110,000 PSI | Passivated, Electropolished, PTFE | Chemical Processing, Cryogenics |
| ASTM A563 | Grade DH / DH3 | 1/2" to 4" | 175,000 PSI | Hot-Dip Galvanized, Mechanical Galvanized | Structural Bolting, Bridge Construction |
| DIN 934 / ISO 4032 Heavy | Class 8.8, 10.9, 12.9 | M3 to M100 | 800 to 1200 MPa | Plain, Geomet, Zinc Flake, Cadmium | Heavy Machinery, Automotive OEM |
The industrial fastener market is undergoing rapid evolution driven by energy transition, offshore automation, and decarbonization mandates. B2B buyers must adapt to emerging material technologies and digital supply chain integration.
Traditional hot-dip galvanizing (HDG) is increasingly being complemented or replaced by high-performance Fluoropolymer PTFE (Xylan) and Zinc-Nickel (Zn-Ni) electroplating. These advanced coatings offer up to 3,000 hours of salt spray resistance (ASTM B117) without causing hydrogen embrittlement or requiring thread over-tapping, preserving maximum proof load integrity in offshore offshore applications.
Modern engineering specifications demand 100% heat-number traceability. Global procurement heads now require direct integration of QR-coded material test certificates (MTC) according to EN 10204 3.1 or 3.2. Additionally, RFID-embedded and strain-sensing heavy hex nuts are gaining adoption in wind turbine bases and subsea manifolds for real-time bolt tension monitoring.
With the European Union's Carbon Border Adjustment Mechanism (CBAM) and global ESG initiatives, top China fastener manufacturers are transitioning to Electric Arc Furnace (EAF) green steel rod inputs. Sourcing heavy hex nuts with verified carbon footprint documentation is becoming a key evaluation parameter for multinational EPC contractors.
Our manufacturing facility utilizes a hybrid production workflow combining multi-station high-speed cold heading machines for high-volume standard sizes and heavy-duty hot forging hydraulic presses for large-diameter (M36 to M100 / 1-1/2" to 4") specialty nuts.
For sizes up to M30 (1-1/8"), our automated 5-station cold headers form heavy hex nuts at rates exceeding 120 pieces per minute. Cold forming forces the grain structure of the steel to follow the contour of the nut body, providing superior fatigue strength and uninterrupted grain flow compared to bar-machined components.
For extreme size ranges or specialized superalloys (such as Inconel 718, Duplex 2205, or Hastelloy C276), our hot forging process heats raw billet stock via precise induction heating to optimal forging temperature windows, eliminating internal void formation and micro-cracking.
To meet the stringent requirements of automated assembly lines, our factory deploys 360-degree laser optical sorting machinery capable of inspecting 100% of finished heavy hex nuts for:
Combining robust manufacturing capacity, accredited testing laboratories, and deep international export experience, we deliver unmatched value to global buyers.
Every batch of heavy hex nuts is stamped with our unique factory logo and material heat code. We supply full EN 10204 3.1 certification detailing chemical analysis (spectrography), yield and tensile strength, hardness (Rockwell C/Vickers), and impact test values (Charpy V-Notch at low temperatures).
Our ISO 17025 accredited laboratory is equipped with 1000kN universal hydraulic tensile test machines, optical emission spectrometers, magnetic particle inspection (MPI) equipment, coating thickness gauges, and automated salt spray corrosion testing chambers.
In addition to standard ANSI B18.2.2 and DIN 934 hex nuts, our engineering team custom-manufactures non-standard heavy hex nuts according to client drawings—including slotted nuts, castle nuts, flange-faced heavy nuts, and self-locking prevailing torque nuts.
Answers to key technical questions asked by procurement directors, quality inspectors, and structural engineers when specifying Chinese heavy hex nuts.