
Explore our premier product portfolio engineered to satisfy strict ASTM, ASME, DIN, and ISO specifications for critical energy applications.
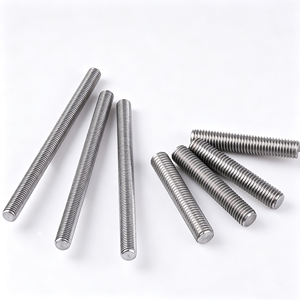
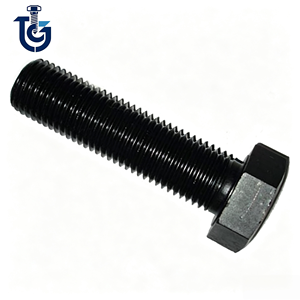
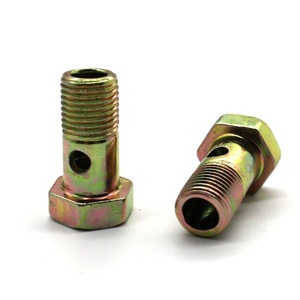
Modern power generation infrastructure operates under extreme physical limits. Thermal power plants, gas turbine combined cycle (CCGT) units, nuclear installations, and offshore wind turbines demand fastening hardware that can resist thermal fatigue, structural vibration, creep deformation, and aggressive chemical oxidation. As a premier China Power Plant Fasteners Factory & Supplier, we engineer high-tensile studs, heavy hex nuts, socket cap screws, and custom flange bolts designed specifically for zero-defect operational continuity.
Fastener failure in power plants accounts for millions of dollars in unscheduled downtime, forced outages, and safety hazards. Mechanical integrity relies heavily on material selection, precision cold and hot forging techniques, microstructural heat treatment, and precise thread geometry. Our factory adheres strictly to international engineering benchmarks including ASTM A193, ASTM A194, ASTM A320, ASTM A453, ASME B16.5, DIN 933/934, and ISO 4014/4017.
Whether servicing high-pressure steam turbines operating at 600°C+, main steam lines, feedwater pumps, or structural condenser frames, our manufacturing processes prioritize grain flow preservation and controlled tensioning characteristics. We provide engineering support from material selection through final torque verification, ensuring long-term operational security for global EPC contractors, plant operators, and maintenance overhaul specialists.
Our vertically integrated manufacturing plant in China combines advanced metallurgy, precision CNC tooling, automated heat treatment, and rigorous quality assurance.
We forge using verified raw materials including ASTM A193 Grade B7/B7M/B16, ASTM A453 Grade 660 (Class A, B, C, D), Inconel 718/625, Nimonic 80A, Stainless 316/347, and Duplex 2205/2507.
Threads are rolled post-heat treatment to maximize fatigue life, eliminate micro-cracks, and maintain tight UN/UNR/Metric tolerances required for hydraulic tensioning systems.
Custom surface treatments including Dacromet, Geomet, PTFE/Xylan, Zinc-Nickel, and Electroless Nickel Plating (ENP) providing outstanding salt spray and anti-galling performance.
Complete quality control dossiers accompanied by Chemical Spectro Analysis, Tensile/Yield Stress Testing, Impact Testing (Charpy V-Notch), Hardness, and NDT (UT/MPI) reports.
Dedicated rapid-response manufacturing units capable of producing custom, non-standard drawing fasteners within accelerated timelines during planned plant turnarounds.
Exporting to over 45 nations with heavy-duty sea-worthy wooden cases, thread protection caps, vacuum moisture barriers, and standardized customs paperwork.
Selecting the optimal steel alloy grade based on thermal limits, mechanical load, and operating environments.
| Material Grade | Standard Specs | Temp. Limit (°C) | Tensile Strength (MPa) | Primary Power Plant Applications |
|---|---|---|---|---|
| ASTM A193 B7 / A194 2H | AISI 4140 Cr-Mo Alloy | -29°C to 425°C | 860 - 1030 MPa | General high-pressure steam flanges, boiler supports, feedwater piping. |
| ASTM A193 B16 / A194 7 | Chromium-Molybdenum-Vanadium | Up to 540°C | 860 - 1030 MPa | Steam turbine casings, main steam stop valves, superheater headers. |
| ASTM A453 Grade 660 (A/B/C/D) | A286 Stainless Superalloy | Up to 700°C | 895 - 1170 MPa | High-temperature gas turbines, steam expansion joints, exhaust flanges. |
| Inconel 718 (UNS N07718) | Ni-Cr Precipitation Hardened | -250°C to 704°C | 1240 - 1400 MPa | Combustion chambers, nuclear reactor internals, ultra-supercritical steam turbines. |
| Stainless Steel 316 / 316L / 347 | Austenitic Stainless Steel | -196°C to 650°C | 515 - 750 MPa | Flue gas desulfurization (FGD) scrubbers, chemical dosing lines, ash handling. |
| Duplex 2205 / Super Duplex 2507 | Austenitic-Ferritic Duplex | -50°C to 300°C | 750 - 1000 MPa | Seawater cooling intakes, nuclear desalination units, offshore wind foundations. |
Modern coal-fired and combined-cycle power plants are transitioning toward Advanced Ultra-Supercritical (A-USC) steam conditions reaching 700°C–760°C and pressures above 35 MPa to maximize fuel efficiency and reduce carbon intensity. This structural shift is displacing traditional ASTM A193 B7/B16 alloys in favor of nickel-base superalloys (such as Inconel 718, Nimonic 80A, and Haynes 282). Procurement teams are prioritizing suppliers with verified vacuum induction melting (VIM) and electro-slag remelting (ESR) raw material sources.
Global environmental mandates (including EU REACH, RoHS 3, and US EPA rules) have severely restricted hexavalent chromium (Cr6+) and cadmium plating. Power plant procurement protocols now demand chromium-free organic zinc flake coatings (such as Dacromet 500LC, Geomet 321), Zinc-Nickel electroplating, and PTFE/Xylan multi-coat systems. These coatings maintain 3,000 to 5,000 hours of neutral salt spray corrosion resistance without risking hydrogen embrittlement in high-strength steels.
The rise of Industry 4.0 predictive maintenance in power plants has accelerated the adoption of RFID-embedded studs and ultrasonic length measurement pins integrated directly into critical turbine casing bolts. Procurement departments are demanding complete digital material passports, where EN 10204 3.1 certificates, heat number logs, non-destructive test (NDT) reports, and torque-tension calibration curves are linked digitally to QR codes or RFID tags for instantaneous job-site verification.
As gas turbine manufacturers migrate toward green hydrogen blending (ranging from 20% to 100% H2 fuel mixtures), power plant engineers are encountering heightened risks of hydrogen-assisted stress cracking (HASC) and high-temperature hydrogen attack (HTHA). Procurement strategies are placing premium value on micro-alloyed, fine-grained vacuum-degassed steels and nickel alloys with strict limits on sulfur and phosphorus impurities.
The manufacturing process for power generation fasteners has evolved beyond simple machining. Achieving long-term resistance against thermal creep fatigue requires advanced processing technologies:
Unlike conventional cut threads or pre-heat-treatment rolling, high-stress turbine studs feature threads rolled after final quenching and tempering. This process induces compressive residual stresses at the root of the thread, increasing fatigue resistance by up to 300% under cyclic steam load vibrations.
Decarburization on fastener surfaces leads to catastrophic micro-cracking under high pressure. Our plant utilizes continuous computer-controlled mesh-belt furnaces with protective nitrogen-endothermic atmospheres, ensuring zero surface decarburization and uniform core hardness.
Modern power plant maintenance relies on hydraulic bolt tensioners rather than manual impact wrenches. Fastener dimensions—especially stud lengths extending beyond the nut, washer face flatness, and thread pitch tolerances—are held to micro-inch precision to accommodate automatic tensioning heads.
We mitigate Hydrogen Embrittlement (HE) and Stress Corrosion Cracking (SCC) through a rigorous three-tier manufacturing process:
The primary differences stem from chemical composition, operating thermal limits, and thermal creep resistance:
Thread rolling is a chipless cold-forming process that reshapes the metal grains along smooth, continuous contours matching the thread profile. In contrast, thread cutting severes the internal metallic grain flow lines, creating sharp stress concentration notches at the root of the thread. Rolled threads offer superior tensile fatigue life, smoother root surface finishes (Rz < 4 µm), and enhanced work-hardened surface layers that resist thread galling during assembly and disassembly.
Every export shipment from our factory is accompanied by a full Quality Dossier compliant with EN 10204 3.1 (or 3.2 third-party inspection by TÜV, SGS, Lloyd's Register upon request). The dossier includes:
PTFE/Xylan coatings significantly reduce the friction coefficient (μ) to a stable, predictable range between 0.08 and 0.12 (compared to 0.15–0.20 for plain or oiled steel). This lower coefficient of friction ensures that a higher percentage of applied torque is converted directly into axial bolt tension (clamp load), reducing torque scatter and preventing thread galling on stainless steel or nickel alloy fasteners. Torque charts must be adjusted when installing PTFE-coated fasteners to prevent over-tightening and premature yield.
Yes. Our China manufacturing facility houses dedicated multi-axis CNC machining centers, heavy forging presses, and tool-making workshops capable of producing custom, non-standard fastners up to M120 (4.75 inches diameter) and lengths up to 3,000 mm. We frequently manufacture custom step studs, heavy hex collar bolts, banjo hollow bolts, spherical washer sets, and turbine casing bolts based on customer CAD/PDF drawings.
Need ASTM A193 B7/B16 studs, Dacromet-coated flange bolts, or custom turbine hardware for your power generation project or maintenance turnaround? Our engineering team is ready to review your specification drawings and provide competitive factory-direct pricing with full material certification.