Marine & Rig
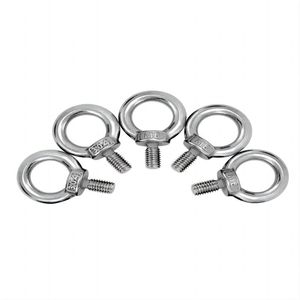
Industrial M5-M12 Stainless Steel Fisheye Eye Bolts Marine Round Head Eyebolt
- Grade: SS304 / SS316 / Duplex
- Size Range: M5 - M12 Heavy Duty
- Application: Marine & Industrial Lifting

Manufactured under strict ISO 9001:2015 & IATF 16949 quality standards with complete mill test traceability (EN 10204 3.1).
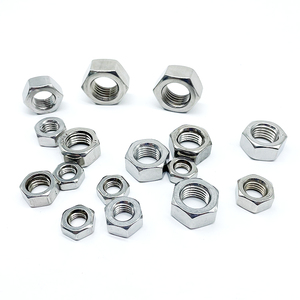
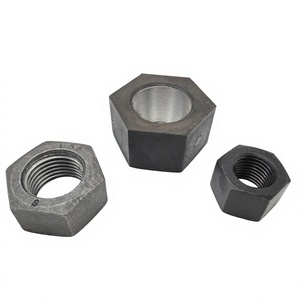
In modern industrial engineering, high-strength structural bolting forms the backbone of critical infrastructure, heavy machinery, automotive powertrains, petrochemical refineries, and wind energy turbines. Among the standard metric property classes defined under ISO 898-1, Grade 10.9 fasteners represent an essential balance of exceptional tensile strength, elevated yield limits, and fatigue endurance. Selecting a certified Grade 10.9 manufacturer requires an in-depth understanding of the metallurgical mechanics, heat treatment cycles, and structural performance tolerances required for safety-critical joints.
The standard numerical designation "10.9" is not an arbitrary code; it directly defines the material's structural performance thresholds:
Critical Engineering Insight: Operating high-tensile fasteners near their yield boundary requires extreme dimensional precision and homogeneous grain structure. Grade 10.9 fasteners display superior resistance to clamp-load relaxation under severe vibrational stress compared to lower class 8.8 alternatives.
To achieve a homogeneous tempered martensite microstructure throughout the entire core cross-section, manufacturers must utilize medium-carbon alloy steels fortified with hardenability elements such as Chromium (Cr), Molybdenum (Mo), Manganese (Mn), and Boron (B). Common raw material grades include AISI 4140, 35CrMo, 42CrMo, 10B21, and 20MnB4.
During quenching in specialized polymer or oil mediums, the steel undergoes a full phase transformation to martensite. Subsequent high-temperature tempering (typically executed above 425°C) relieves residual internal stress while maintaining strict core-to-surface hardness thresholds (typically 320 to 380 HV or 32 to 39 HRC). This precise microstructural refinement ensures high impact energy absorption, even at sub-zero working temperatures down to -40°C.
Engineering teams frequently evaluate Grade 10.9 against Grade 8.8 and Grade 12.9 fasteners to determine the ideal safety margin and weight optimization for structural frames. Below is an expert comparative matrix highlighting mechanical property metrics under ISO 898-1 and ASTM equivalents.
| Property Class | Nominal Tensile (MPa) | Yield Strength 0.2% (MPa) | Core Hardness (HRC) | Elongation A5 (%) | Charpy V Impact (-20°C) | Hydrogen Risk |
|---|---|---|---|---|---|---|
| Grade 8.8 | 800 MPa | 640 MPa | 22 - 32 HRC | ≥ 12% | ≥ 30 Joules | Low |
| Grade 10.9 | 1000 MPa | 900 MPa | 32 - 39 HRC | ≥ 9% | ≥ 27 Joules | Moderate - Controlled |
| Grade 12.9 | 1200 MPa | 1080 MPa | 39 - 44 HRC | ≥ 8% | ≥ 15 Joules | High - Baking Req. |
Achieving the correct clamp force (preload) without over-torquing or yielding the fastener thread requires precise calculation based on thread friction coefficient (μ = 0.12 to 0.14 for standard zinc electroplated or oiled surfaces). The table below details engineered torque recommendations for metric Grade 10.9 coarse thread bolts:
| Thread Size (Coarse) | Thread Pitch (mm) | Tensile Stress Area (mm²) | Proof Load (kN) | Preload / Clamp Force (kN) | Rec. Tightening Torque (N·m) |
|---|---|---|---|---|---|
| M8 | 1.25 mm | 36.6 mm² | 30.4 kN | 24.3 kN | 35 N·m |
| M10 | 1.50 mm | 58.0 mm² | 48.1 kN | 38.5 kN | 70 N·m |
| M12 | 1.75 mm | 84.3 mm² | 70.0 kN | 56.0 kN | 120 N·m |
| M16 | 2.00 mm | 157.0 mm² | 130.0 kN | 104.0 kN | 295 N·m |
| M20 | 2.50 mm | 245.0 mm² | 203.0 kN | 162.0 kN | 580 N·m |
| M24 | 3.00 mm | 353.0 mm² | 293.0 kN | 234.0 kN | 1000 N·m |
| M30 | 3.50 mm | 561.0 mm² | 466.0 kN | 372.0 kN | 1980 N·m |
The global fasteners market is witnessing a major transformation driven by renewable energy expansions, electric vehicle (EV) lightweighting, and automated smart manufacturing. Purchasing managers and EPC directors must align with suppliers offering forward-looking production technologies.
Environmental regulations (REACH & RoHS) are accelerating the phase-out of hexavalent chromium plating. Factories are moving toward Geomet and Dacromet micro-layer zinc flake coatings offering 1,500+ hours of neutral salt spray protection without hydrogen embrittlement risks.
Wind power OEMs and high-speed rail operators are deploying "Smart Bolts" equipped with embedded piezoelectric ultrasonic micro-transducers and RFID chips for non-destructive real-time tension measurement during maintenance.
Leading Grade 10.9 factories employ high-speed glass turntable vision systems to check 360-degree pitch diameter, head concentricity, and crack detection, guaranteeing ZERO defects (PPM < 1) for automated robotic assembly lines.
As an ISO-certified direct manufacturer and global supplier, our infrastructure is engineered to satisfy the rigorous technical requirements of international EPC contractors, oil & gas refineries, automotive Tier-1 suppliers, and structural engineering firms.
Every production batch originates from verified top-tier steel mills with original Mill Test Reports. We execute 100% Positive Material Identification (PMI) using handheld XRF spectrometers upon arrival. Heat numbers are stamped on the bolt heads along with grade identification markings, ensuring 100% full lifecycle traceability back to the melt furnace.
Our quality control center operates under strict ISO/IEC 17025 laboratory guidelines, equipped with state-of-the-art destructive and non-destructive testing machinery:
Beyond standard DIN 931, DIN 933, ISO 4014, and ASME B18.2.1 fasteners, our CNC machining center produces non-standard fasteners according to customer blueprints. Whether you require custom collar flanges, non-standard pitch threads (UNF, UNEF, Fine Metric), extended lengths up to 3,000 mm, or special high-temperature alloy grades (Super Duplex, Inconel 718, Monel K-500), our engineering team provides rapid prototyping and production scale-up.
Addressing core technical questions from procurement officers, quality control auditors, and structural engineers regarding Grade 10.9 fasteners procurement.
Grade 10.9 signifies a high-tensile metric property class under ISO 898-1. The number '10' indicates a minimum nominal tensile strength of 1,000 MPa (Megapascals). The '.9' indicates that the yield point is 90% of the tensile strength, equal to a minimum yield strength of 900 MPa. These fasteners are designed for heavy-duty structural applications requiring maximum clamping load.
Because Grade 10.9 bolts have a hardness exceeding 32 HRC (approx. 320 HV), atomic hydrogen absorption during acid pickling or electroplating poses a high risk of catastrophic brittle failure under tension. We mitigate this by executing a mandatory post-plating de-embrittlement baking process in specialized baking ovens at 190°C to 220°C for 4 to 24 hours within 4 hours after electroplating. Alternatively, we recommend non-electrolytic coatings such as Geomet or Dacromet.
Welding Grade 10.9 alloy steel fasteners is generally NOT recommended because the high localized heat alters the tempered martensite microstructure, leading to micro-cracking and severe reduction in yield strength. Regarding Hot-Dip Galvanizing (HDG), it must be performed with controlled high-temperature galvanizing processes and specialized spin-centrifuging to clear threads, followed by hardness verification to ensure thermal tempering did not occur during the molten zinc bath (450°C).
While both are high-strength alloy fasteners, ASTM A193 Grade B7 is primarily an inch-series (and metric conversion) specification intended for high-temperature and high-pressure pressure vessel and valve flange applications (Chromium-Molybdenum steel). ISO 898-1 Grade 10.9 is a metric structural property class for general mechanical engineering, automotive, and heavy construction. Mechanical strength values are similar (B7 tensile is ~125 ksi / 860 MPa yield min vs Grade 10.9 900 MPa yield min).
Every shipment is accompanied by a full EN 10204 3.1 Material Test Certificate (MTC) containing raw material chemical ladle analysis, mechanical tension test values, hardness profiles, impact energy readings, surface coating thickness reports, and dimensional inspection logs. Third-party inspection reports (TUV, SGS, Bureau Veritas, Lloyd's Register) are available upon request.
For aggressive coastal or offshore installations, we provide PTFE / Xylan fluoropolymer coatings, Zinc-Nickel alloy electroplating (withstanding 1,500+ hours salt spray test), Geomet 321/500 silver flake finish, Hot-Dip Galvanizing (HDG) per ISO 1461, and passivated stainless steel or Duplex alloys for total immunity to rust.
For standard stock sizes (e.g., DIN 931 / DIN 934 Grade 10.9 M6 to M36 in Black Oxide or Zinc finish), orders ship within 3 to 7 business days. For customized OEM drawings, specialized threading, or custom coatings, typical production lead time ranges from 15 to 25 days depending on batch volume. We accommodate small-batch sample testing as well as multi-container EPC project shipments.
All threads are cold-rolled for smooth grain flow and maximum fatigue life. Threads are checked using calibrated Go / No-Go thread ring gauges adhering to ISO 965-2 6g tolerance classes (or 2A/3A for imperial threads). For high-volume automated feeds, 100% optical vision sorting machines screen out minor thread nicks or pitch errors.
Grade 10.9 bolts are heavily specified in Automotive Chassis & Powertrain Systems, Wind Turbine Hub & Tower Assemblies, Heavy Construction Machinery (Excavators & Cranes), Structural Steel Frameworks (Bridges & Stadiums), Mining Equipment, and Railway Locomotive Bogies.
You can click the "Inquire Now" button on any product card or click the CTA button below to submit your detailed RFQ (including grade, size, coating, thread pitch, and quantity). Our sales engineering team responds within 2 hours with detailed factory-direct pricing and technical datasheets.
Partner with an ISO 9001:2015 certified manufacturer. Get factory-direct pricing, complete EN 10204 3.1 material traceability, and rapid global delivery across 24+ countries.
Inquire Now