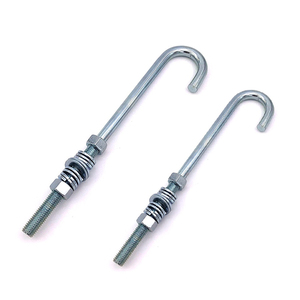

Explore our ISO 9001 certified full thread stud bolts, anchor bolts, hex nuts, and high-strength fasteners manufactured to ASTM, ASME, and DIN standards for immediate dispatch to Chicago project sites.
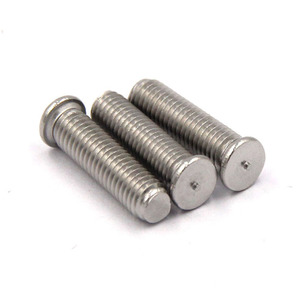
The Greater Chicago Metropolitan Area (Chicagoland)—spanning Cook County, Will County, and the broader Midwest industrial corridor—remains one of North America's primary epicenters for heavy manufacturing, oil refining, chemical processing, structural steel erection, and maritime transport. Securing reliable, high-yield, and fatigue-resistant full thread studs is a fundamental engineering requirement for plant operations managers, procurement officers, and structural engineers throughout the region.
As a premier China wholesale full thread studs manufacturer and global exporter serving Chicago, our manufacturing facilities combine advanced cold-heading, CNC precision thread rolling, continuous heat treatment, and automated surface barrier coating. We produce industrial stud bolts capable of handling severe pressure differentials, thermal cycling, and harsh environmental exposure unique to the Great Lakes climate.
In Midwestern industrial applications, temperature swings from -20°F in winter to over 95°F in summer induce intense micro-strain and relaxation on flanged joints. Standard machine bolts often suffer thread shear or clamp-load degradation. Full thread studs distribute axial stress uniformly across their entire engagement length, eliminating localized stress risers under thermal expansion and dynamic mechanical vibration.
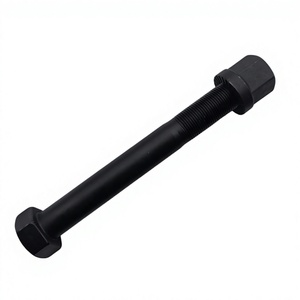
Full thread studs (also designated as continuous thread stud bolts under ASME B18.31.2) are engineered without an unthreaded body shank. This design optimizes stress distribution across the entire bolt length when locked by heavy hex nuts at both ends (conforming to ASTM A194 Grade 2H, Grade 8, or Grade 8M). Depending on your operational environment—whether high-pressure refining in Whiting, structural bridge assembly under IDOT oversight, or sub-zero gas storage facilities—selecting the proper material grade is crucial.
Below is a reference guide for engineering teams selecting full thread studs for Chicago project bids:
| Specification Grade | Material Category | Tensile Strength (Min PSI) | Yield Strength (Min PSI) | Operating Temp Range | Target Chicago Industry Use Case |
|---|---|---|---|---|---|
| ASTM A193 Grade B7 | AISI 4140/4142 Cr-Mo Alloy | 125,000 PSI | 105,000 PSI | -20°F to 1000°F | Petrochemical Refineries, Heat Exchangers, Flange Valves |
| ASTM A193 Grade B16 | Chromium-Molybdenum-Vanadium | 125,000 PSI | 105,000 PSI | -20°F to 1100°F | Steam Power Boilers, High-Temp Pressure Vessels |
| ASTM A320 Grade L7 | AISI 4140 Quenched & Tempered | 125,000 PSI | 105,000 PSI | -150°F to 700°F | Cold-Climate Pipelines, Sub-Zero Gas Storage (Chicagoland) |
| ASTM A193 Grade B8 Cl.2 | AISI 304 Stainless (Strain Hardened) | 110,000 PSI | 95,000 PSI | -325°F to 1500°F | Food & Beverage Processing, Hygienic Chemical Piping |
| ASTM A193 Grade B8M Cl.2 | AISI 316 Stainless (Strain Hardened) | 110,000 PSI | 95,000 PSI | -325°F to 1500°F | Marine Hardware, Deicing Salt Exposed Infrastructure |
| UNS S32750 Super Duplex | 25Cr-7Ni-4Mo-N Stainless | 116,000 PSI | 80,000 PSI | -40°F to 600°F | Chloride-Rich Wastewater Treatment, Heavy Industrial Scrubbers |
Our OEM manufacturing capabilities are designed to meet the rigorous demands of Chicago’s diverse industrial infrastructure:
Supplying ASTM A193 B7/B7M studs with PTFE/Xylan fluoropolymer coatings for refinery expansions along the Calumet River and Northwest Indiana refining complexes. Anti-galling coatings ensure smooth breakout torque during maintenance turnarounds.
Heavy-duty continuous thread rods and foundation studs manufactured to IDOT (Illinois Department of Transportation) and AASHTO structural requirements. Hot-Dip Galvanized (HDG) finishes protect against aggressive road deicing salt exposure.
Full thread studs engineered in ASTM A320 L7 and Grade B8M Class 2 for commercial refrigeration units, district heating loops, and cold-chain distribution warehouses operating across Chicagoland logistics hubs.
Untreated alloy fasteners exposed to Chicago’s severe humidity, lakefront atmospheric moisture, and industrial emissions can experience rapid oxidation and thread lockup. As an expert OEM exporter, we offer specialized protective surface treatments tailored to your operational environment:
Procuring full thread studs directly from our factory in China yields a 25% to 40% cost efficiency compared to local stocking distributors, while maintaining strict adherence to North American engineering standards. We manage end-to-end logistics to the Greater Chicago market:
Combining high-capacity automated production with metallurgical precision to back Chicago’s critical projects.
We source raw steel bars exclusively from top-tier certified steel mills. Every single heat is logged, chemically verified, and traceable from raw bar to final packed stud bolt.
Thread profiles are formed via cold thread rolling rather than cutting. This preserves grain flow continuity, improves surface finish, and enhances fatigue life under cyclic loads.
We routinely coordinate third-party inspections with SGS, TUV, Bureau Veritas (BV), or Lloyd's Register to verify dimensions, hardness, and coating thickness prior to export shipping.
Answers to common technical, metallurgical, and logistical questions from Chicagoland engineering and procurement departments.
Full thread studs (continuous thread) offer significant mechanical advantages in flanged piping and pressure vessel joints. Unlike standard hex bolts, which concentrate tension at the unthreaded-to-threaded junction under load, a full thread stud distributes elastic elongation across its entire length. This minimizes strain concentration, reduces clamp-load relaxation during thermal cycling, and allows easy removal during maintenance even if exposed ends experience corrosion or thread damage.
We manufacture stud bolts according to ASME B1.1 standards. For imperial sizes up to 1 inch, Unified Coarse (UNC) threads are standard. For stud diameters 1-1/8 inch and above, 8-Thread Series (8-UN) is typically specified for high-pressure ASME B16.5 flange connections. Metric full thread studs conforming to DIN 975 / DIN 976 and ISO metric pitch standards are also available in full stock.
Standard carbon or high-tensile steel fasteners can undergo a ductile-to-brittle transition when exposed to sub-zero temperatures (such as Chicago winter lows of -15°F to -25°F). Our ASTM A320 L7 stud bolts are specifically heat-treated and subjected to Charpy V-Notch impact testing at -150°F (-101°C), guaranteeing a minimum impact energy absorption of 20 ft-lbs (27 Joules). This prevents sudden brittle fracture in outdoor pipelines, structural frameworks, and refrigeration equipment.
Every shipment is delivered with a comprehensive Quality Assurance Dossier, including: EN 10204 3.1 Material Test Certificates (MTRs), Chemical Composition Analysis, Tensile and Yield Strength Reports, Elongation and Hardness Verification, Charpy Impact Test Reports (for A320), Plating/Coating Thickness Certificates, and Packing Lists with Heat Number cross-referencing.
Production lead time typically ranges from 10 to 18 days depending on order volume and specialized coating requirements. Transit options include express air freight for urgent shutdown spares (3 to 5 days to O'Hare International Airport) and ocean vessel freight via West Coast ports or direct Midwest intermodal rail hubs (18 to 25 days to Chicago distribution centers).
Yes. In addition to standard ASME B18.31.2 sizes, our CNC machining centers can turn and thread custom stud lengths, chamfered end profiles, stepped thread studs, and non-standard thread pitches in exotic materials such as Inconel, Monel, Hastelloy, and Titanium Grade 5 based on your CAD drawings or engineering datasheets.
Need high-tensile ASTM A193 B7 studs, stainless steel threaded rods, or PTFE-coated flanged fasteners? Contact our engineering sales team today for factory-direct wholesale pricing, material datasheets, and lead-time schedules.