
Explore our specialized inventory of high-tensile, corrosion-resistant, and elevated-temperature industrial fasteners manufactured strictly to ASME, ASTM, DIN, and API standards.
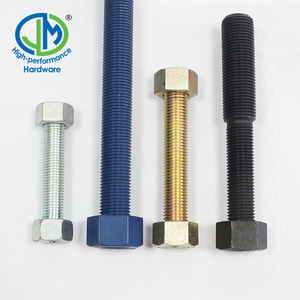
The Greater Seattle region, encompassing key petroleum refining hubs across King, Skagit, and Whatcom counties (including industrial centers near Anacortes, Ferndale, and Cherry Point), represents one of the most critical energy and marine petrochemical nodes in the Pacific Northwest. Petroleum refineries operating along Puget Sound operate under stringently monitored microclimates characterized by high humidity, marine aerosol exposure, cyclic thermal fatigue, and heavy regulatory oversight from the Washington State Department of Ecology and EPA Region 10.
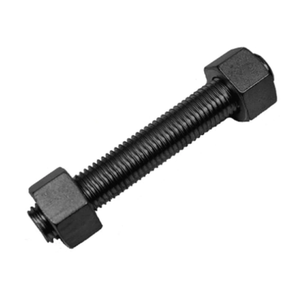
Maintaining joint integrity across high-pressure cracking units, hydrotreaters, catalytic reformers, crude distillation units (CDUs), and offshore marine loading terminals requires fastener solutions that transcend standard commercial grades. As an established global manufacturer and direct exporter of refinery-grade bolting systems, we supply custom-machined and standard ASTM A193, ASTM A194, ASTM A320, and corrosion-resistant nickel-alloy stud bolts engineered to withstand the dual challenges of extreme process metallurgy and coastal salt-spray degradation.
Information Gain Insight: Flange leakage in refinery pressure boundary systems accounts for over 45% of unscheduled turnaround downtime. In coastal refineries such as those in Puget Sound, galvanic corrosion between carbon steel pipe flanges and improperly coated alloy fasteners accelerates crevice oxidation. Deploying fluoropolymer PTFE (Xylan)-coated ASTM A193 B7 studs paired with ASTM A194 Grade 2H heavy hex nuts reduces friction co-efficients down to 0.08, guaranteeing consistent bolt preload and zero-emissions clamping force.
Refineries operating near the Salish Sea face distinct operational stresses due to the interaction of high-temperature refinery streams and atmospheric marine moisture. Bolt integrity must be assured across three primary thermal and chemical operational zones:
In hydrodesulfurization (HDS) and catalytic reforming units, process piping operates at temperatures exceeding 1,000°F (538°C) under high hydrogen partial pressures. Standard carbon steel studs experience creep strain and thermal relaxation, leading to loss of gasket stress. We manufacture ASTM A193 Grade B16 chromium-molybdenum-vanadium alloy steel stud bolts specifically engineered for high-temperature service. The addition of vanadium ensures microstructural stability and high creep-rupture strength over extended 4-to-6 year refinery run-lengths.
Ocean-facing docks, crude oil unloading jetties, and coastal vapor recovery systems in Seattle undergo perpetual salt fog exposure. Standard hot-dip galvanized fasteners often suffer from hydrogen embrittlement when high-strength steels (hardened above 32 HRC) are acid-pickled. Our facility utilizes advanced Zinc-Nickel Electroplating (ASTM B841) and Multi-Layer PTFE Fluoropolymer Coating Systems that provide over 3,000 hours of salt spray resistance per ASTM B117 standards without compromising thread engagement tolerance.
Liquefied LPG/LNG transfer facilities and subsea cryogenic lines require fasteners that retain impact toughness at sub-zero temperatures. We supply ASTM A320 Grade L7 (quenched and tempered alloy steel tested to -150°F / -101°C) and ASTM A320 Grade L43 (L7M for sour gas environments), alongside strain-hardened austenitic stainless steels like ASTM A193 Grade B8M Class 2 for subsea and freezing-ambient flange assemblies.
Engineers and procurement specialists in Seattle refineries rely on precise material selection based on operating envelope conditions. Below is a engineering matrix highlighting common grades exported to Pacific Northwest projects:
| Specification Grade | Material Composition | Tensile Strength (Min) | Yield Strength (Min) | Recommended Temp Range | Primary Seattle Application |
|---|---|---|---|---|---|
| ASTM A193 B7 | Chromium-Molybdenum (AISI 4140/4142) | 125,000 PSI (860 MPa) | 105,000 PSI (720 MPa) | -20°F to 800°F (-29°C to 427°C) | High-pressure ASME B16.5 pipe flanges, crude distillation units. |
| ASTM A193 B16 | Cr-Mo-V Alloy Steel | 125,000 PSI (860 MPa) | 105,000 PSI (720 MPa) | -20°F to 1100°F (-29°C to 593°C) | Coker units, steam methane reformers, high-temp boilers. |
| ASTM A193 B8M (Cl. 2) | AISI 316 Stainless (Strain Hardened) | 110,000 PSI (760 MPa) | 95,000 PSI (655 MPa) | -325°F to 1500°F (-198°C to 816°C) | Coastal washdown zones, marine docks, acidic chemical pumps. |
| ASTM A320 L7 | AISI 4140 Quenched & Tempered | 125,000 PSI (860 MPa) | 105,000 PSI (720 MPa) | Charpy tested down to -150°F (-101°C) | Refrigerated LPG transfer lines, cryogenic process loops. |
| Inconel 625 (UNS N06625) | Nickel-Chromium-Molybdenum-Columbium | 120,000 PSI (827 MPa) | 60,000 PSI (414 MPa) | -320°F to 1800°F (-196°C to 982°C) | HF Alkylation units, severe wet chlorine & sour gas (NACE MR0175). |
| Duplex 2205 (UNS S31803) | 22% Cr, 5% Ni, 3% Mo Duplex SS | 95,000 PSI (655 MPa) | 65,000 PSI (450 MPa) | -50°F to 600°F (-46°C to 315°C) | Desalination units, sour water strippers, marine heat exchangers. |
Thread galling during installation is a major cause of flange assembly failure when using austenitic stainless steel or nickel alloys. In critical turnaround schedule (TAR) windows, a single galled stud can delay hydrotesting by several hours. Our manufacturing facility applies high-performance surface treatments engineered for smooth torque application and total environmental protection:
Every single stud bolt, heavy hex nut, and custom machined threaded component exported to the Seattle market undergoes comprehensive testing inside our ISO/IEC 17025 accredited laboratory. We provide full material certification in compliance with EN 10204 3.1, detailing physical properties, chemical analysis, heat treatment charts, and non-destructive testing results.
Our quality verification protocol includes:
Combining primary manufacturing efficiency with rigorous international export expertise to deliver reliable bolting systems directly to Pacific Northwest ports.
Our integrated forging and thread rolling facility enforces rigorous process control from raw billet selection through final export crating.
All studs and nuts are hard-stamped with mill heat numbers and material grade codes, fully backed by certified chemical/mechanical test reports.
Pre-packaged flange bolt kits tailored to specific ASME B16.5 pipe sizes, ensuring fast turnaround replacement during scheduled refinery shutdowns.
Direct export logistics with custom wooden palletizing, anti-rust oil paper wrapping, and express customs handling for hassle-free delivery to Port of Seattle and Port of Tacoma.
Clarifying technical specs, export compliance, lead times, and application suitability for Northwest industrial buyers.
Bare ASTM A193 B7 alloy steel studs are susceptible to rapid surface rusting in humid, high-salinity air. For Seattle-area installations, we recommend specifying our Blue PTFE (Xylan 1424) coated or Zinc-Nickel plated B7 studs. These coatings block corrosive airborne salt ions, prevent crevice corrosion under gaskets, and maintain low breakout torque even after extended exposure to Pacific Northwest ocean fogs.
Yes. For sour oil and wet H2S refining processes, we supply ASTM A193 Grade B7M and ASTM A194 Grade 2HM fasteners, as well as Nickel Alloy 625 and Monel K-500 studs. Grade B7M fasteners undergo specialized heat treatment to restrict maximum hardness to 22 HRC, preventing sulfide stress cracking (SSC) in accordance with NACE MR0175 directives.
We maintain extensive stock of standard ASTM A193 B7, B16, and Stainless B8/B8M stud bolts ranging from 1/2" to 3.5" in diameter. Emergency air-freight orders can be processed, packaged, and dispatched to Seattle-Tacoma International Airport (SEA) within 48 to 72 hours. Standard ocean container shipments typically arrive at the Port of Seattle within 20 to 25 calendar days.
Absolutely. In addition to standard ASME B18.31.2 stud bolts and ASME B18.2.2 heavy hex nuts, our CNC machining center produces custom double-end studs, collar bolts, extra-long anchor bolts, and specialized rigging clamps in exotic alloys like Titanium Grade 5, Hastelloy C276, and Super Duplex UNS S32750 tailored exactly to your CAD drawings.
Every shipment is delivered with a complete export document package including: EN 10204 3.1 Material Test Reports (MTRs) tracing original melt mill heats, chemical and mechanical inspection certificates, coating thickness test reports, packing lists, commercial invoices, and Certificate of Origin (COO).
Our technical sales team specializes in high-temperature, high-pressure, and marine-corrosion bolting applications. Submit your project requirements today for immediate pricing and material verification.
Inquire Now